2026 Best Pump Lubrication Systems for Global Buyers
Selecting the right pump lubrication system can determine whether a pump runs smoothly or fails during a critical production cycle. In 2026, global buyers face more choices, but not every system suits every operating environment. Temperature, viscosity, contamination, speed, load, maintenance access, and local service support must guide the decision.
Jim Fitch, founder of Noria Corporation and a recognized lubrication reliability expert, stated, “Lubrication is the lifeblood of machinery.” That principle remains practical on the plant floor. A properly designed pump lubrication system can deliver controlled lubricant flow, reduce friction, limit heat buildup, and protect bearings during demanding operation. Small details matter. A blocked line, incorrect grease, or poorly positioned reservoir can undermine an expensive installation.
This guide compares leading pump lubrication solutions for international buyers in 2026. It considers automatic grease systems, oil circulation units, oil mist systems, and hybrid arrangements. Each option brings advantages, limitations, and maintenance requirements. Some systems perform well in clean factories but struggle near dust, water, or chemical vapors. Others offer excellent monitoring but require skilled installation and reliable spare parts.
Real-world selection is rarely perfect. Budget pressure can encourage shortcuts. Those shortcuts may become costly later. Buyers should verify technical data, compatibility, certification needs, warranty terms, and after-sales support before ordering. Supplier claims also deserve careful checking. Performance depends on installation quality, lubricant condition, operating discipline, and inspection records. The best choice is not always the most advanced system. It is the system that remains reliable, serviceable, and measurable in the buyer’s actual environment.
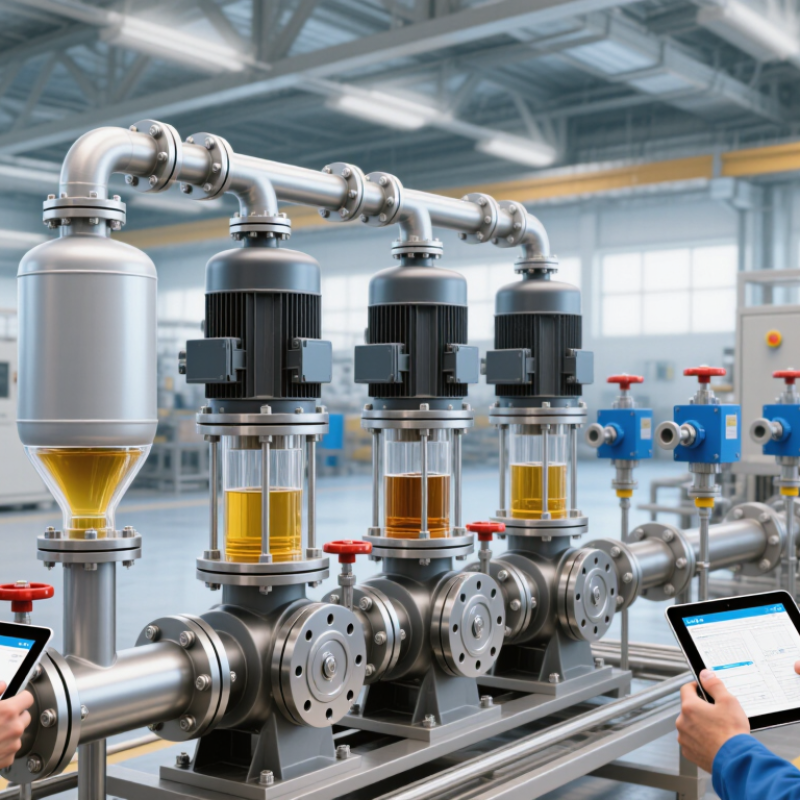
Pump Lubrication System Types Classified by ISO 6743-4
Global pump buyers should treat ISO 6743-4 as a fluid classification tool, not a complete hardware standard. It groups hydraulic lubricants by performance and composition. HH oils provide basic protection. HL fluids add oxidation and rust resistance. HM fluids emphasize anti-wear performance, while HV fluids support wider temperature changes. The difference matters beside a hot pump casing or a cold outdoor start.
Fire-resistant categories require closer review. HFAE and HFAS use high water content. HFB refers to water-in-oil emulsions. HFC fluids use water-polymer solutions. HFD fluids are water-free and usually demand stricter seal and material compatibility checks. ISO 6743-4 helps narrow selection, but it does not replace viscosity checks, cleanliness targets, or pump-maker instructions. A label is not a design.
The U.S. Department of Energy reports that pumping systems can represent about 27% of industrial electricity use in its Improving Pumping System Performance sourcebook. That figure makes lubrication efficiency a purchasing issue, not a minor maintenance detail. Field experience shows that over-greasing can raise bearing temperature within minutes. Under-lubrication leaves noisy bearings and metallic dust around the seal area. Buyers should compare operating temperature, load, water exposure, relubrication intervals, and ISO 4406 cleanliness requirements. The European Lubricating Grease Institute also stresses consistency selection through NLGI grades, yet grade alone cannot predict compatibility. I would still request a compatibility test. Procurement teams sometimes trust the datasheet too quickly.
Oil Flow and Cooling Design Under API 614 Requirements
2026 Best Pump Lubrication Systems for Global Buyers
Oil Flow and Cooling Design Under API 614 Requirements
API 614 treats lubrication as a protection system, not a simple oil supply. Global buyers should examine flow paths, standby capacity, filtration, cooling, and alarm logic together. Oil must reach every bearing with stable pressure and suitable viscosity. Keep it clean. During field inspections, blocked filters often reveal more risk than undersized pumps. The system should normally include a main pump, an automatically available standby pump, and suitable pressure control. Each transition must avoid sudden oil starvation. Many specifications mention redundancy but explain little about switching behavior. That gap deserves attention.
Cooling design starts with the operating environment. Select a cooler for the required heat load, expected fouling, and local cooling-water conditions. A dual cooler arrangement can support maintenance without stopping the equipment. Place temperature measurement near the oil supply to the machine, not only at the reservoir. Oil temperature changes quickly after load increases. Coolers with poor venting can trap air and reduce performance. On hot sites, a theoretical margin may disappear during summer operation. Do not rely on average weather data.
Reliable systems also depend on commissioning discipline. Flush piping until particle levels meet the project’s cleanliness target, then verify flow at operating temperature. Record pressure, temperature, and filter differential readings. Small deviations become useful baseline data. Alarm testing should include low pressure, high temperature, pump failure, and high filter differential. Operators need clear response instructions. One uncomfortable lesson is that complex systems can be harder to maintain. API 614 alignment should support safe inspection, practical access, and predictable recovery after a component fault.
Grease Versus Oil Lubrication Using ISO 281 Bearing Life Ratings
2026 Best Pump Lubrication Systems for Global Buyers
Grease versus oil lubrication should be assessed through ISO 281 bearing life ratings. ISO 281 calculates basic rating life, L10, from bearing load and fatigue capacity. Lubricant choice influences the modified rating life through viscosity, contamination, and operating conditions. It is not a lubricant score.
Grease stays put.
It suits sealed bearings, slower shafts, and equipment needing simple maintenance. A suitable grease can maintain an adequate viscosity ratio, κ, while reducing leakage risks. However, excessive grease may create churning, heat, and higher starting torque. In field inspections, over-greasing is a common and costly mistake.
Oil runs cooler.
Oil circulation can remove heat from high-speed pump bearings and carry particles toward filtration. It often supports stable lubrication when temperature, speed, and cleanliness are tightly controlled. Yet seals, reservoirs, filters, and oil analysis add complexity. ISO 281 results can look attractive while real contamination shortens service life.
Global buyers should compare the calculated L10 and modified life under actual load, speed, temperature, and cleanliness conditions. Request viscosity data at operating temperature, not only at 40°C. Check relubrication intervals and storage conditions. A neat calculation can still fail. Real machines are less tidy than spreadsheets. When oil supply is uncertain, a well-selected grease system may provide more dependable field performance than a theoretically superior oil arrangement.
2026 Selection Matrix for Speed, Load, Temperature, and Contamination
2026 Best Pump Lubrication Systems for Global Buyers
2026 Selection Matrix for Speed, Load, Temperature, and Contamination
Pump lubrication selection should begin with operating evidence, not catalogue labels. The U.S. Department of Energy reports that pumping systems can consume about 25% of industrial electricity. Its Pumping System Assessment Tool also identifies 20–50% saving potential in many inefficient systems. Lower friction helps, but incorrect lubricant viscosity can increase heat and energy demand. High-speed pumps usually need lower viscosity and reliable oil circulation. Heavy loads require stronger films and carefully verified additive chemistry.
Temperature changes the decision quickly. For hot service, select an oil with a high viscosity index and confirmed oxidation stability. For cold starts, check the actual starting torque, not only the running temperature. ISO 4406:2021 provides a practical contamination coding method for fluid cleanliness. A pump operating near water, dust, or metal debris needs sealed reservoirs, breathers, and routine particle checks. Small particles matter.
The matrix should compare speed, load, temperature, and contamination together. One field study may suggest a suitable grade, but site conditions can disagree. I have seen clean oil fail after a poor breather choice. That mistake is easy to miss. Buyers should request test data for viscosity, demulsibility, rust protection, and filterability. ASTM D1401 and ASTM D892 methods can support these checks. Still, no matrix replaces oil sampling, vibration trends, and a review of the pump’s actual duty cycle.
Global Compliance Checks: ATEX, IECEx, CE, UL, and ISO Documentation
For global buyers, pump lubrication systems need more than a technical datasheet. ATEX applies to equipment intended for explosive atmospheres in the European Union. IECEx offers an internationally recognized certification route, but acceptance still depends on local regulations. CE marking requires a valid conformity assessment and technical file. UL certification or recognized testing may support North American procurement, especially where site rules require an approved electrical enclosure.
Check the nameplate, zone rating, gas or dust group, temperature class, and ambient range. Inspect cable glands, seals, control voltage, and lubricant compatibility. IECEx certificates should match the exact model and protection concept. ATEX documents should identify the equipment category and applicable harmonized standards. ISO 9001 does not certify explosion protection. It demonstrates controlled quality processes. The ISO Survey 2022 recorded 1,265,216 ISO 9001 certificates across 189 countries and economies, showing its global relevance. Still, paperwork can hide weak engineering. A certificate is not a risk assessment.
Tips: Request the declaration of conformity, certificate schedule, drawings, test reports, and revision history. Compare every document with the delivered unit. Keep translations controlled. Ask who accepts the file locally. This small step is often missed. Procurement teams should also verify maintenance instructions, inspection intervals, and spare-part traceability. Incomplete records may delay commissioning, even when the hardware appears suitable.